SABRE | SBR/SBX
Cleanroom High Bay for Extreme Environments
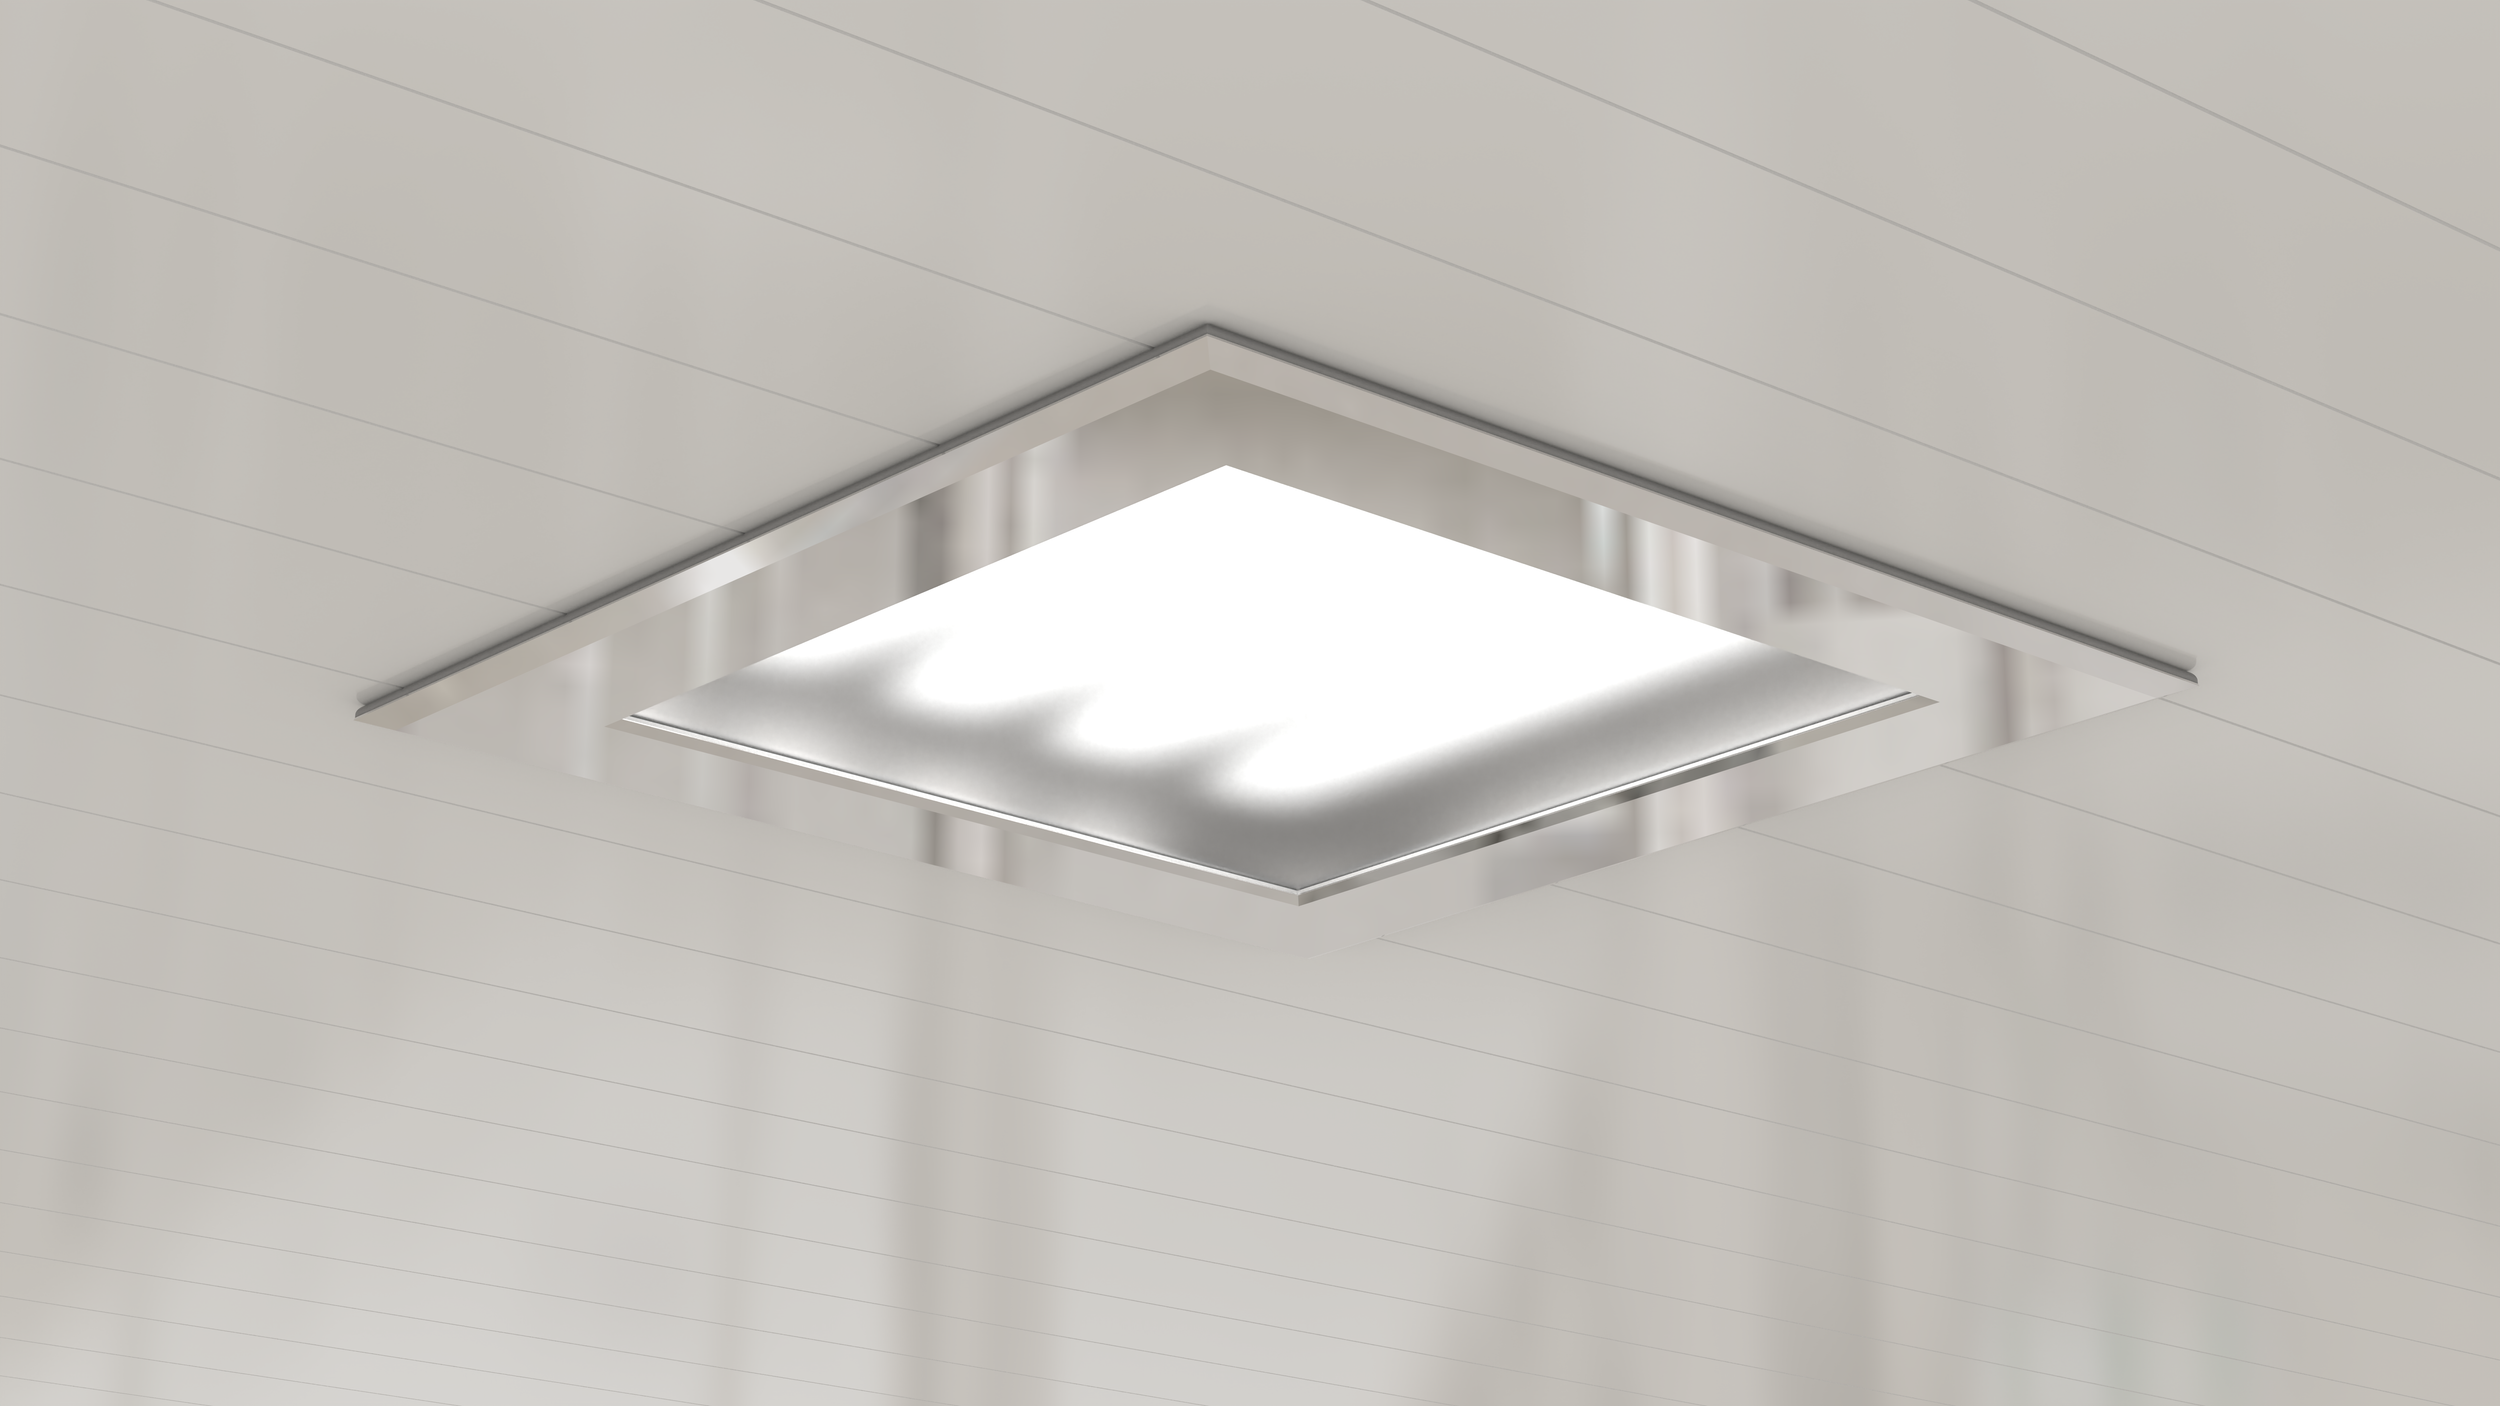
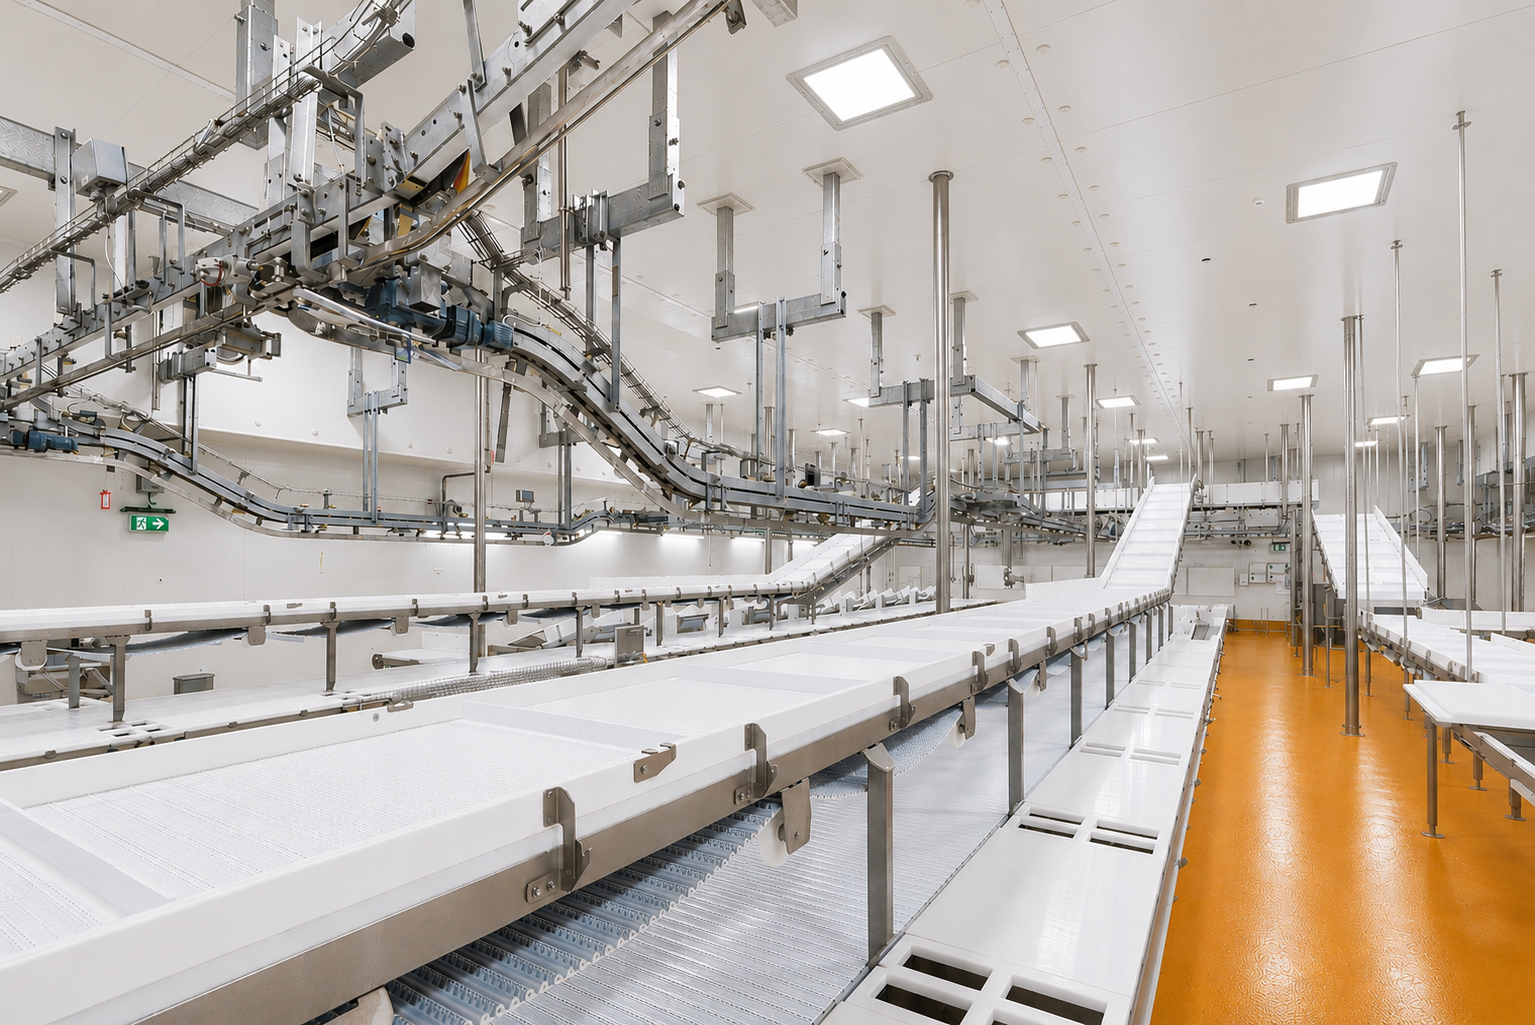
Building on the success of the Isollux Soffito range, Sabre™ delivers a heavy-duty recessed cleanroom luminaire for food processing and industrial production where continuous rising steam, hydrolytic conditions, elevated ambient temperatures or exceptionally high light outputs exceed the practical operating limits of conventional recessed hygienic luminaires.
Manufactured to order, Sabre is available in standard configurations to simplify upgrades to existing installations, with engineering support for bespoke dimensions, power, material selection and environmental requirements.
Chemical, Steam & Hydrolytic Resistance
Sabre can be configured with materials and sealing systems selected to withstand continuous steam, extreme humidity, hydrolytic stress and aggressive sanitation environments.
Steam CIP
Extreme Humidity and Hydrolytic Stress
High Ambient Sanitation
Customise to your requirements
Facilities operating at elevated ambient temperatures, requiring high illumination from significant mounting heights, or constrained by existing building structures often exceed the practical capabilities of conventional recessed luminaires.
Sabre can be specified and configured to suit site-specific requirements, including bespoke dimensions, increased power and light output, remote driver topologies and materials selected for task-critical operating environments.
If a standard configuration does not meet your project requirements, our engineering team is on hand to assist with the development of a bespoke solution.
Service Life
Long service life depends on conservative engineering rather than driving components to their limits.
Sabre combines independently verified LM-80 testing, TM-21-21 reported lumen maintenance projections and conservatively operated high-density LED arrays to deliver predictable long-term performance.
L85 > 10 Years 24/7
Isollux XE dual-die LED chipsets are conservatively operated to optimise service life and deliver L80 (B0) >102,000 h within the published operating limits of the specified configuration.
Explore how we engineer and validate LED performance
Long - Term Maintenance
Unlike conventional sealed LED luminaires, Sabre's permanent stainless-steel enclosure is designed to remain part of the building throughout the life of the facility. Serviceable LED engines and drivers can then be replaced or upgraded as components age or technology evolves, extending the practical life of the installation while reducing waste, disruption and total cost of ownership.
Find out more about engineering for extreme environments
Optimised Visual Comfort & Safety
Sabre’s high-density LED arrays and diffuse optics eliminate harsh point-light sources and high-intensity reflected glare from white and stainless steel surfaces.
Soft, uniform illumination reduces shadows around complex machinery, improving visibility for safer operation, inspection, cleaning and maintenance.
Colour Rendering Options
CRI 85 and CRI 95 are available as standard, with options up to CRI 97 and custom spectrum control for specialised inspection, production and process requirements.
Find out more about our LED Options and Performance
Product Configurations
The following specifications relate to the standard 600 × 600 mm SBR/SBX configuration.
120W | 18,000lm
150 W | 22,500lm
180 W | 27,000lm
360 W | 54,000lm (Custom Format)
Sabre SBX | Lift-Out LED & Lens Assembly
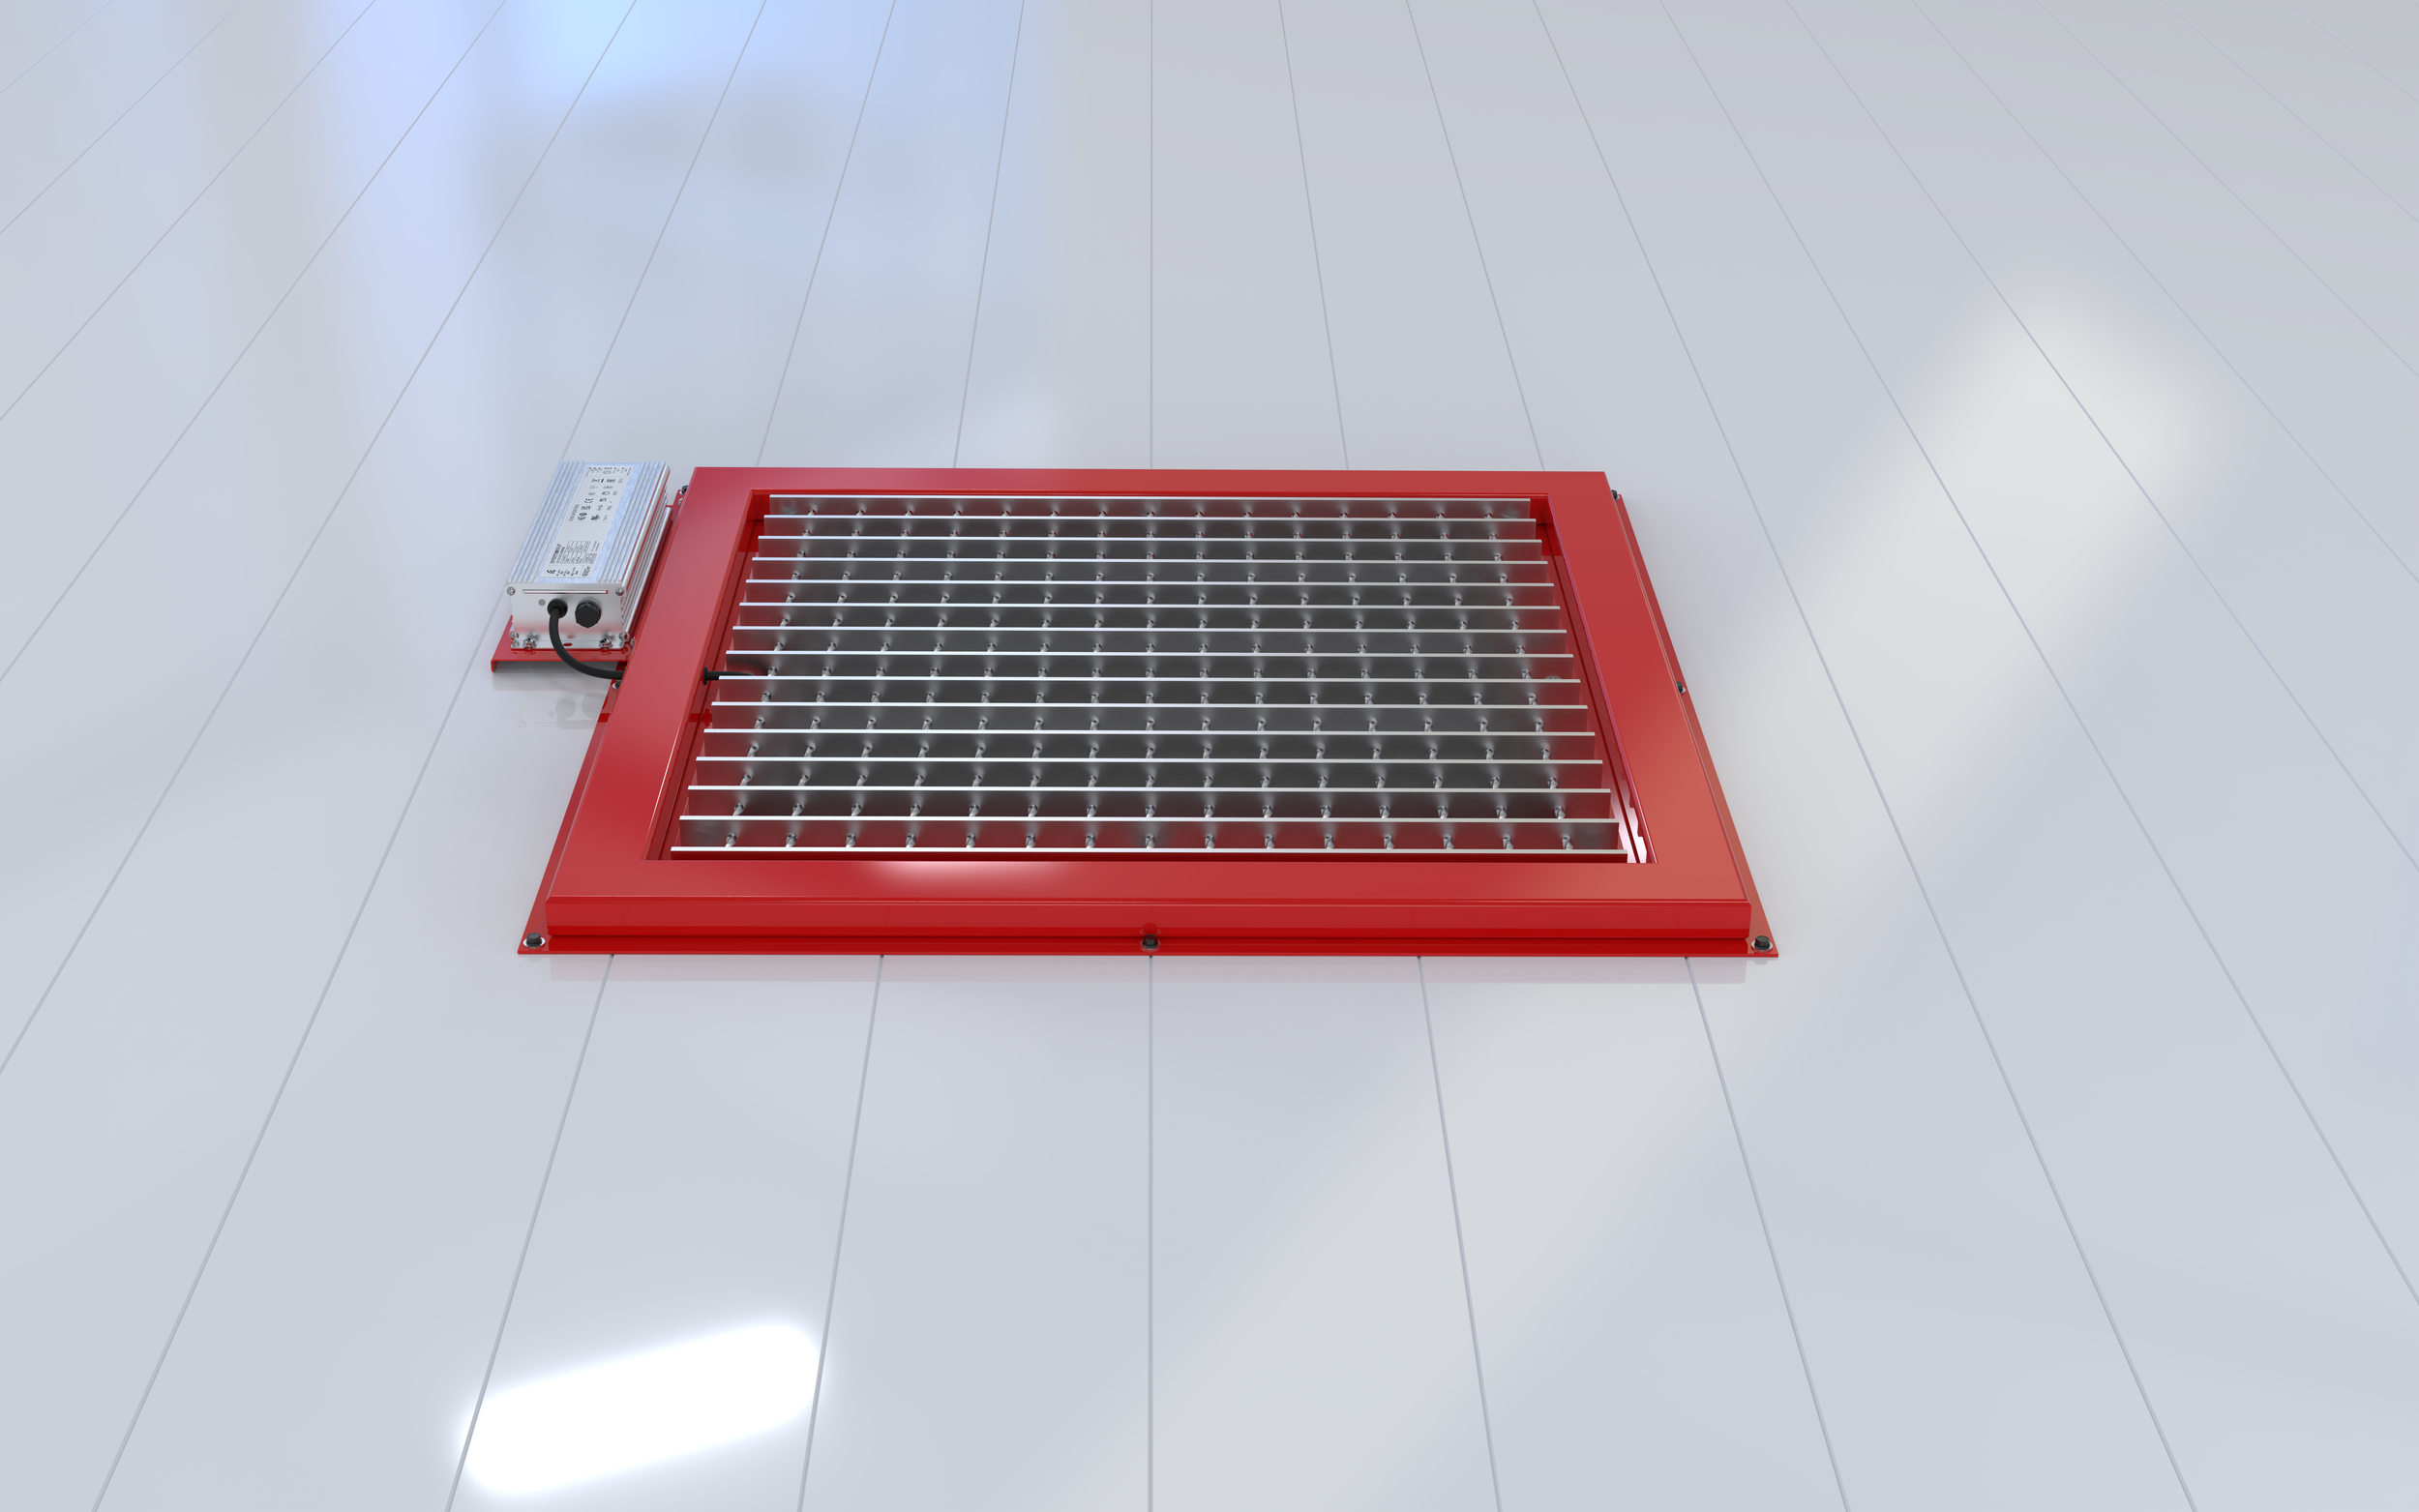
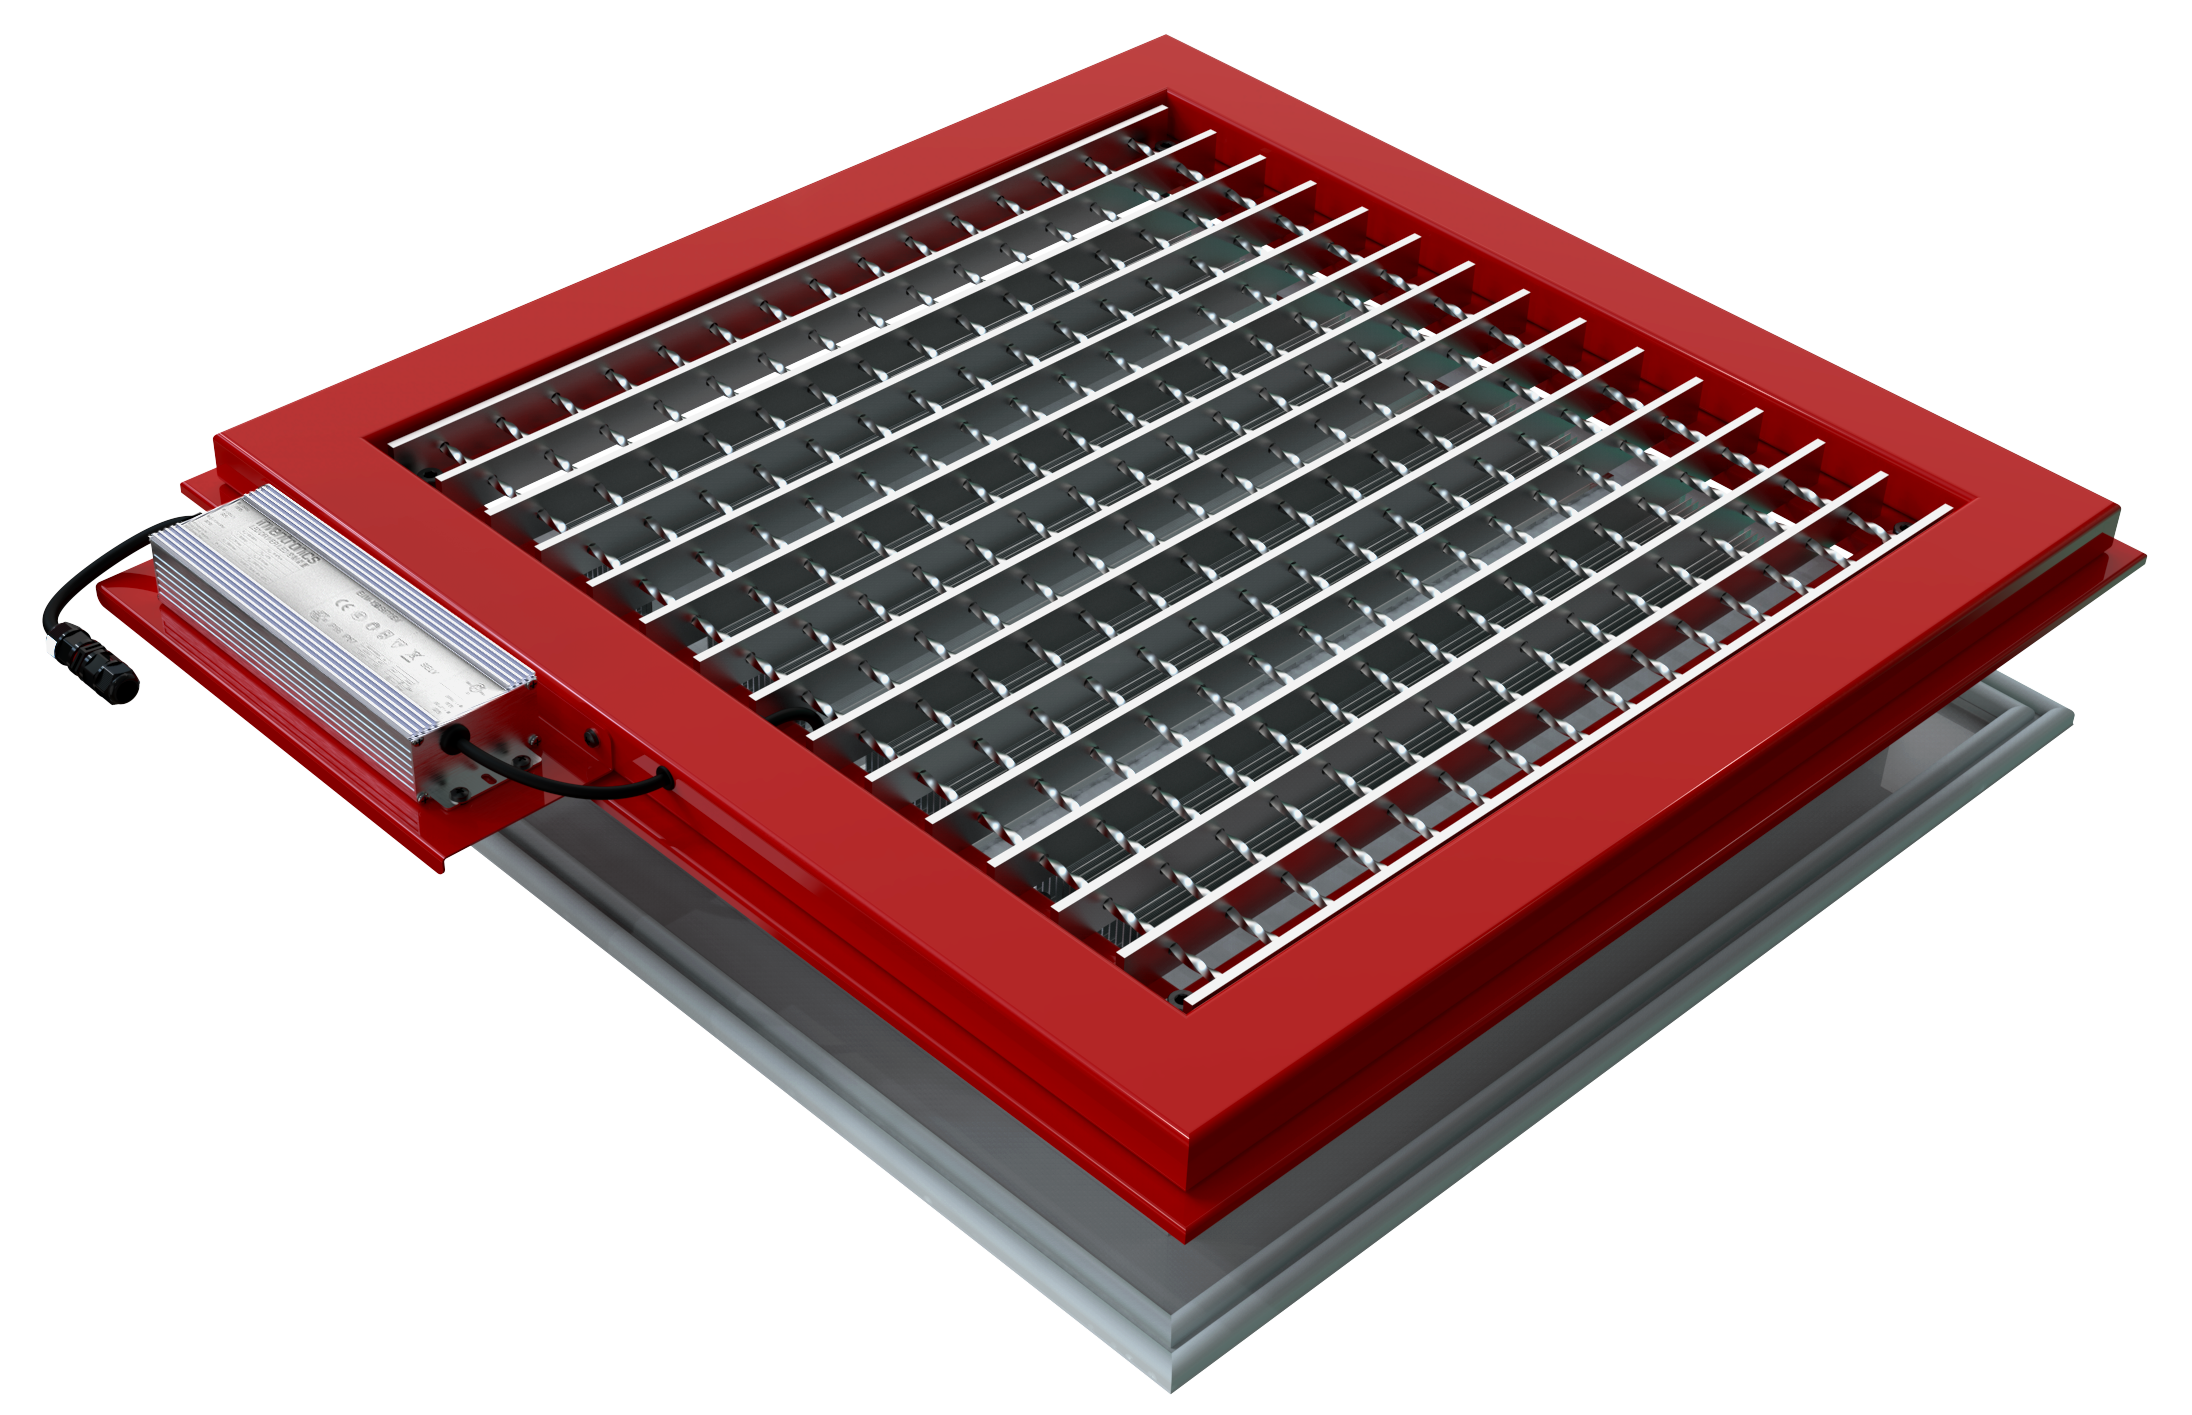
The LED light engine, lens and retaining frame form a single sealed removable assembly that can be removed in minutes for cleaning or servicing away from the production area.
Ideal where grease, fats or dust progressively reduce light transmission and routine maintenance forms part of the cleaning programme.
Sabre SBR | Fixed Lens Assembly
The lens remains permanently sealed within the stainless steel frame while the LED engine is removed independently from above. The lens is normally cleaned from below and only removed when replacement is required.
Ideal where preserving the room-facing hygienic seal is the priority while maintaining a fully serviceable lighting system.
Contact our technical team for support with specification
Common Product Features
The following features relate to both SBR and SBX
L85 > 10 Years | 24/7 Operation
Anti-Vibration
Serviceable Architecture
High-Density XE LED Array
Remote Driver Options
Emergency Options
Ingress Protection
Impact Resistance
EPDM or Bespoke Seals
EPDM sealing systems are standard for most food processing, pharmaceutical and hygienic wash-down applications. Where exposure to specialist chemicals, oils, fuels, solvents or other aggressive process media is anticipated, alternative sealing materials can be specified to suit the application.
Ingress Protection
Sabre provides a minimum IP66 ingress protection, with configurations available up to IP69K on the room-facing side for high-pressure wash-down and sanitation environments.
Lighting Controls
Sabre supports simple dual-circuit switching together with DALI control options for dimming, sensing, tunable white and multi-channel spectrum control.
Emergency Lighting
Options include a 30 W / 90-minute emergency pack, an auxiliary 30 W driver to reduce UPS load, or DALI control to assign selected luminaires to an emergency scene.
Electrical Protection
Sabre features independent SELV drivers, de-rated to 80% of maximum output to reduce component stress and extend service life. Drivers may be remotely mounted up to 300 m from the luminaire where maintenance access is restricted or elevated ambient temperatures require electrical equipment to be located outside the operating environment.
Protection includes:
- Min IP66 Independent SELV drivers
- IP67 Power Connection
- Flicker-Free Output
- Under-Voltage Protection
- Over-Voltage Protection
- Short-Circuit Protection with auto recovery
- Over-Temperature Protection
- Wide Input Range 90–305VAC
- Surge Protection – DM 6kV, CM 10kV
- Driver Class I & Class II hazardous locations

Recommended Lens Specification
| M1 | M2 | M3 | |
|---|---|---|---|
| Continuous Fryers | ● | ○ | ○ |
| Continuous Cookers | ● | ○ | ○ |
| Steam Tunnels | ● | ○ | ○ |
| CIP Processing | ● | ○ | ○ |
| Heavy Industry (Chemical) | ● | ○ | ○ |
| Pharmaceuticals | ● | ○ | ○ |
| Sanitisers | ● | ● | ○ |
| Meat and Poultry | ● | ● | ○ |
| Dairy | ● | ● | ○ |
| Beverage | ● | ● | ○ |
| High-Output Non-Chemical | ○ | ○ | ● |
| Hygiene & Packaging | ○ | ● | ● |
| General Food Processing | ○ | ● | ● |
| Commercial Kitchens | ○ | ● | ● |
| Industrial Processing | ○ | ● | ● |
● Recommended
○ Application Dependent
Chemical Resistance
M1 provides the highest level of chemical, temperature and hydrolytic resistance, including direct steam exposure.
M2 uses the proven TPX material system for demanding food-processing chemicals and sanitisers, while M3 polycarbonate is suited to applications where aggressive chemical exposure, elevated temperatures and hydrolytic stress are not primary concerns.
M2 has been tested against elevated concentrations of the active ingredients listed below; M1 PPSU provides equal or greater resistance for these applications.
| Active Ingredient | |
|---|---|
| Acetic Acid | 64-19-7 |
| Ethoxylated Alcohols | Mixture |
| Amines | Mixture |
| Benzalkonium Chloride | 8001-54-5 |
| Benzyl Alkyldimethyl Chlorides | Mixture |
| Disodium Metasilicate | 6834-92-0 |
| Dodecyldimethylamine Oxide | 1643-20-5 |
| Ethanol | 64-17-5 |
| Hydrogen Peroxide | 7722-84-1 |
| Hypochlorous Acid | 7790-92-3 |
| Peracetic Acid | 79-21-0 |
| Potassium Hydroxide | 1310-58-3 |
| Quaternary Ammonium Compounds (QACs) | Mixture |
| Secondary Alkanesulphonates | Mixture |
| Sodium Carbonate | Mixture |
| Sodium Dodecylbenzene Sulfonate | 25155-30-0 |
| Sodium Hydroxide | 1310-73-2 |
| Sodium Hypochlorite | 7681-52-9 |
Contact Us for the Full Data Pack